


Bespoke solutions for twin walled re-enforced pipes in deeper installations
If the municipal sewerage network or the plant pipeline on the premises runs deep underground, the separator must be buried to the appropriate depth. This is the only way to ensure the necessary gradient. Similarly, complex changes in ground level or multi-storey underground car parks can pose a challenge if the installation point lies metres below ground level. In such cases, the basis for bespoke solutions is a PE twin walled re-enforced pipe, within which the grease separator is housed together with an accessible plant room in a single structure.
The separate plant room provides space for a lifting station or pumping equipment, the control system, measurement equipment and sampling points. This ensures that all technical equipment is always housed in a dry and frost-proof environment. Nevertheless, access is always possible: several manhole covers allow entry into the interior to carry out regular maintenance work.
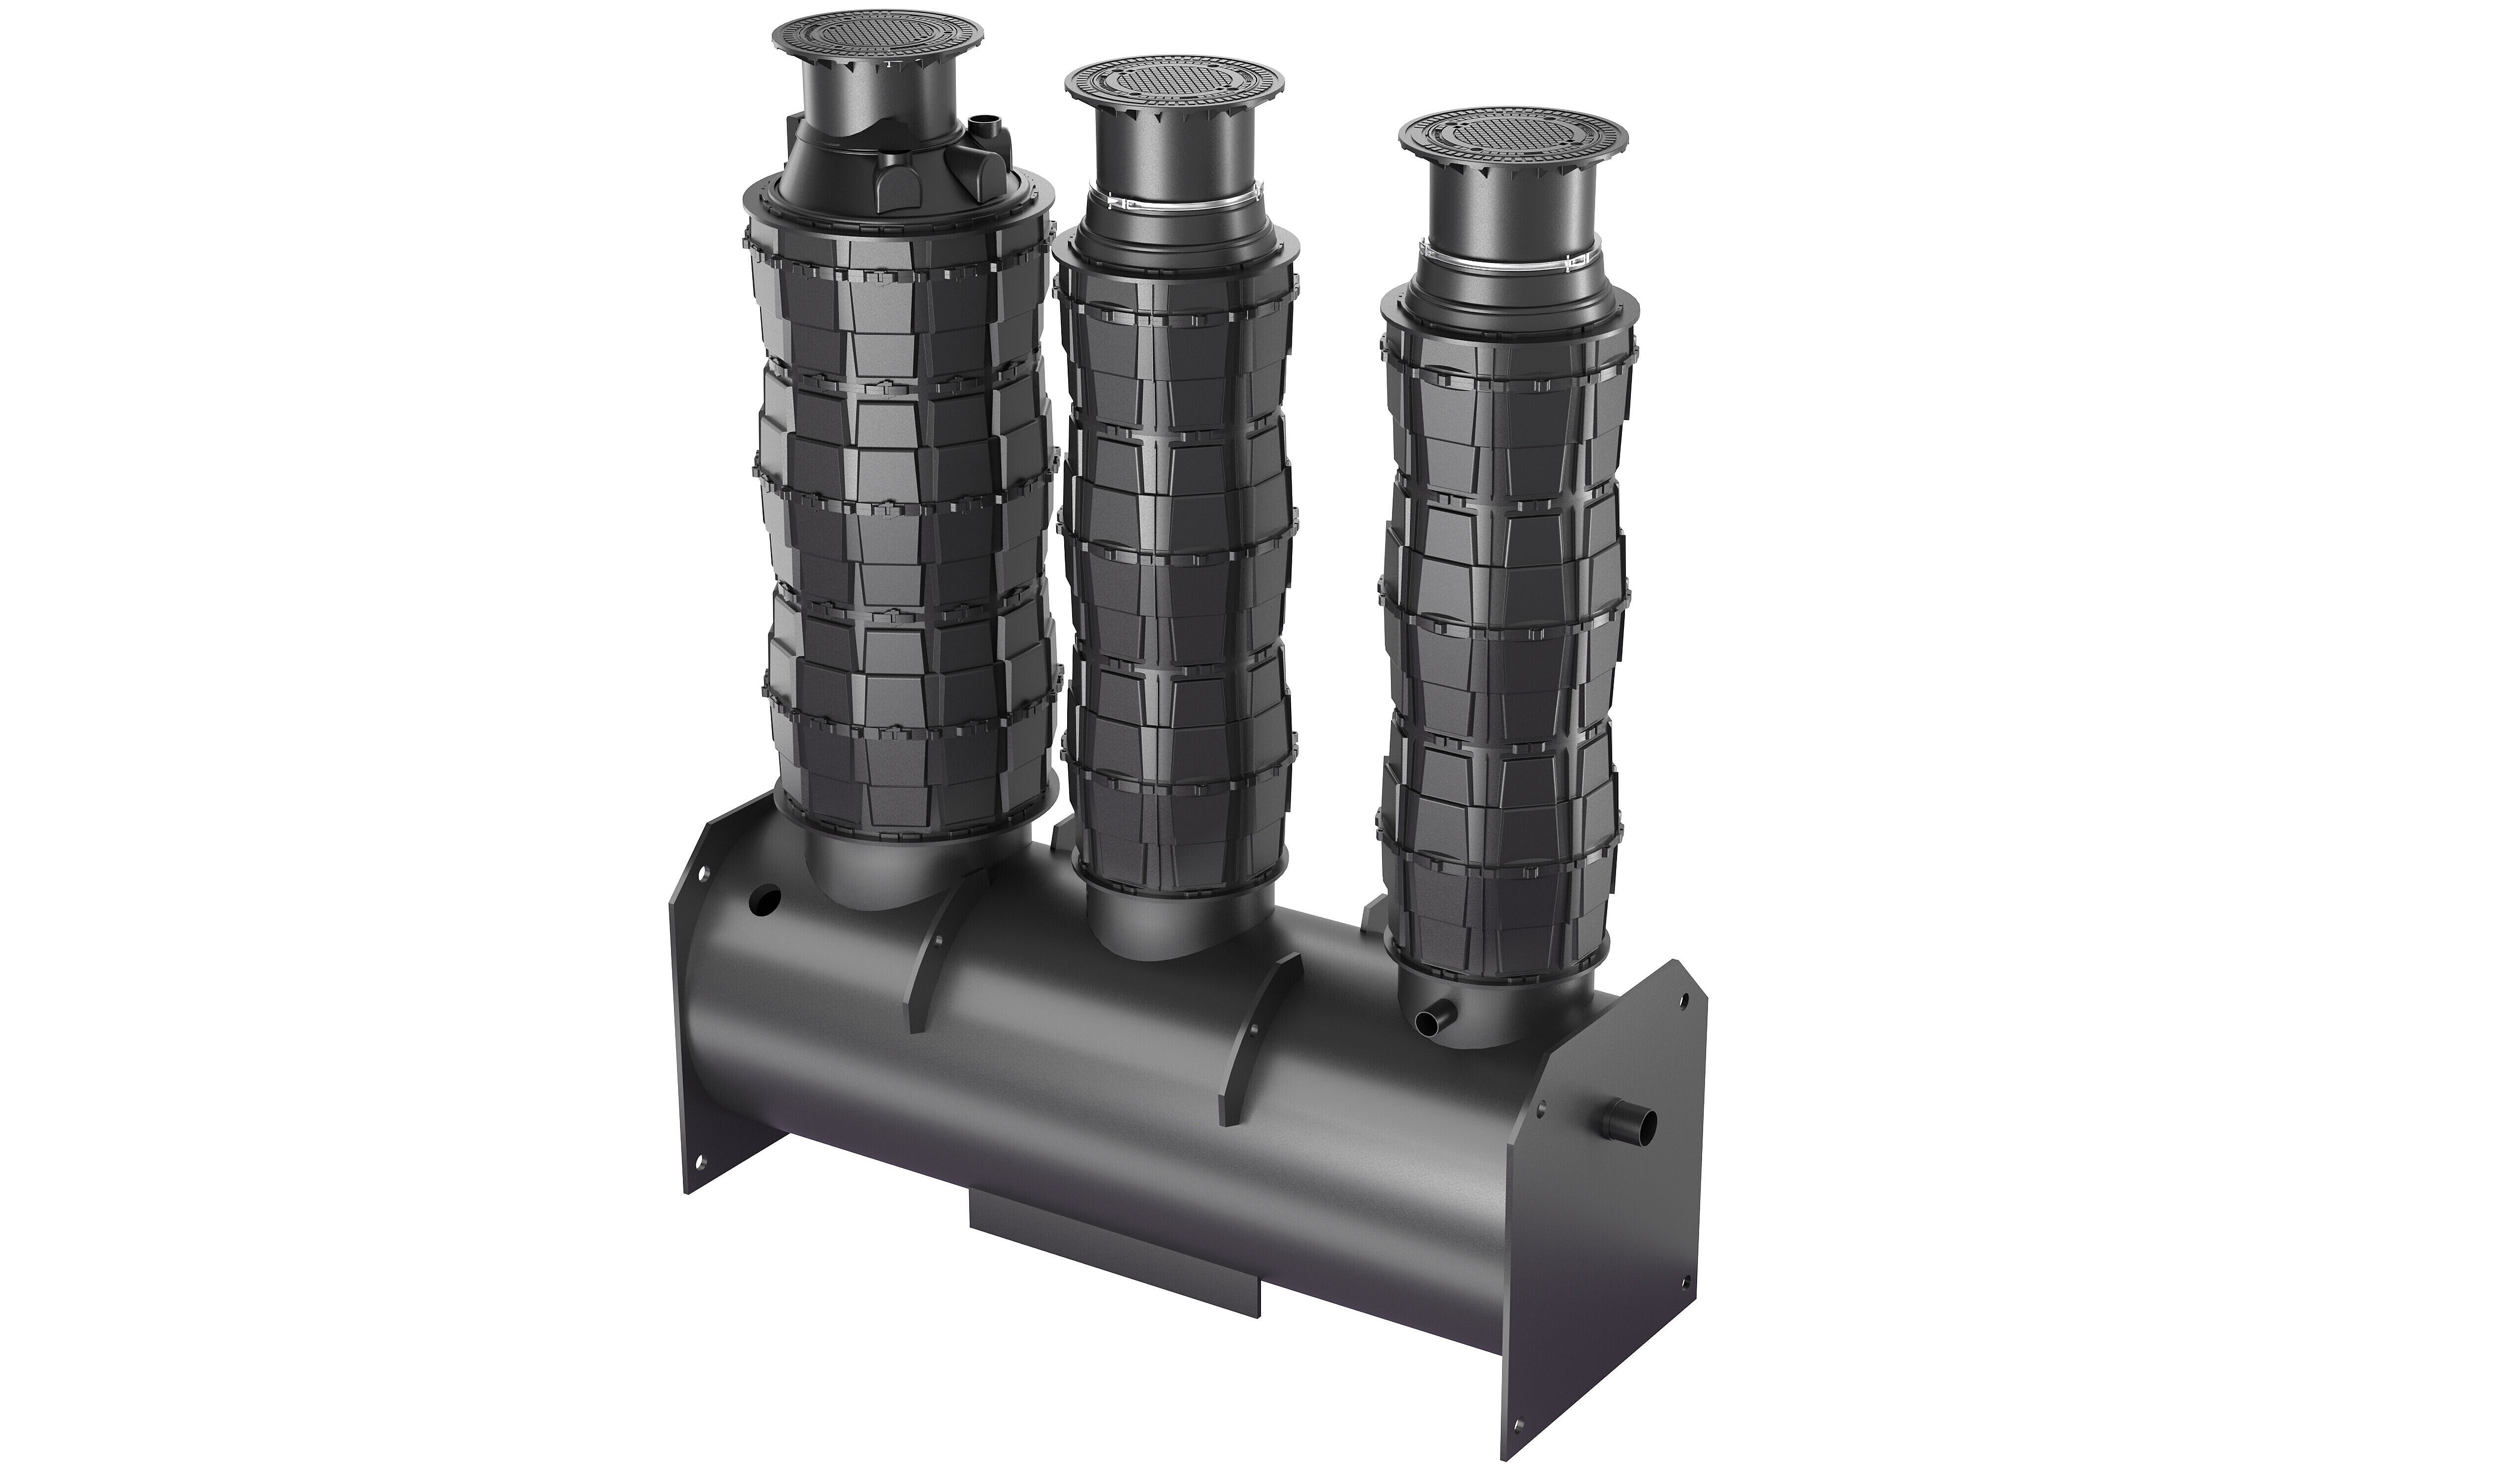
Very deep drainage
Where drainage pipes run at very great depths, this presents particular challenges for designers and developers. As wastewater must flow by gravity, a deep sewer connection necessitates the appropriate installation of separators and manholes. This requires bespoke solutions in the form of structurally robust tanks within the most stable spiral-wound pipe systems possible, in order to withstand earth pressure and groundwater.
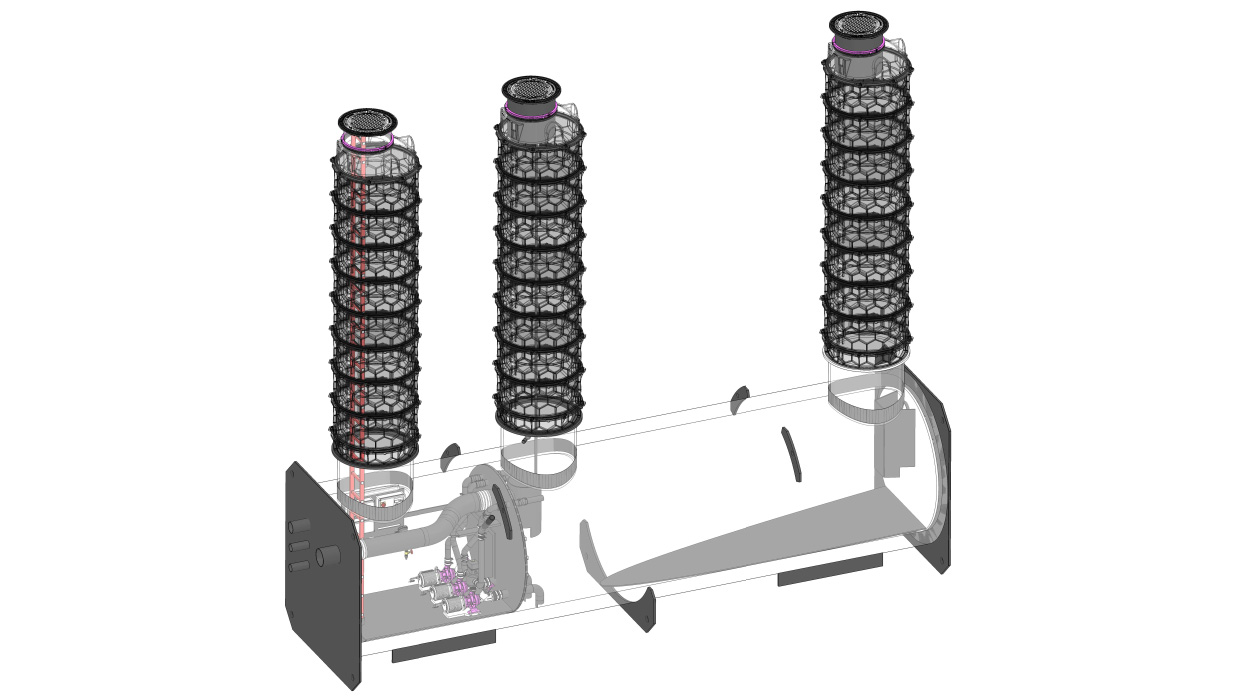
Large feed depths
Standard prefabricated tanks often have fixed installation heights. Bespoke solutions made from robust twin walled re-enforced pipe offer a precise solution to this problem: they are manufactured to fit the structural geometry and the required base depth exactly. This eliminates the need for unnecessary intermediate shafts, ensures structural safety against earth pressure, and allows wastewater to drain away smoothly and continuously.

Installation in an area with groundwater
The installation of a grease separator in an area with groundwater is technically feasible without any problems. However, this requires professional planning and special structural measures. In particular, measures to prevent buoyancy and the loads caused by hydrostatic pressure call for bespoke solutions. Pressure-resistant and dimensionally stable bespoke designs ensure that groundwater is reliably prevented from entering the system and that wastewater is reliably prevented from escaping.
lack of space
If there are no cellars or plant rooms available for free-standing installation, or if regulatory or hygiene requirements prohibit installation inside food processing premises, butchers’ shops or catering establishments, the separator system must be installed underground. Customised twin walled re-enforced pipe shaft structures are the ideal solution when greater installation depths are required.
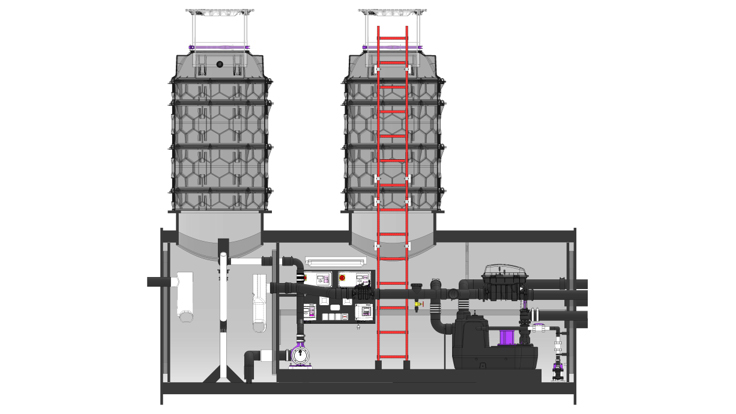
Optimal accessibility
The twin walled re-enforced pipe made of polyethylene accommodates both the grease separator and all the associated technical equipment. Easy access to all components is particularly important, especially where installation depths are considerable. A separate technical room offers many advantages in this context: as well as providing dry and secure accommodation, it also allows maintenance to be carried out without opening the grease separator. Depending on the requirements, customised combinations with direct disposal, a lifting station and sampling are possible.

KESSEL quality from Lenting
Our team is here to work with you to determine the specifications your bespoke product must meet. We then design, manufacture and test your custom-made product in our development department in Lenting and, if required, install it on site. That’s KESSEL service all under one roof: expert, personalised and efficient.